 Datum Design Journal
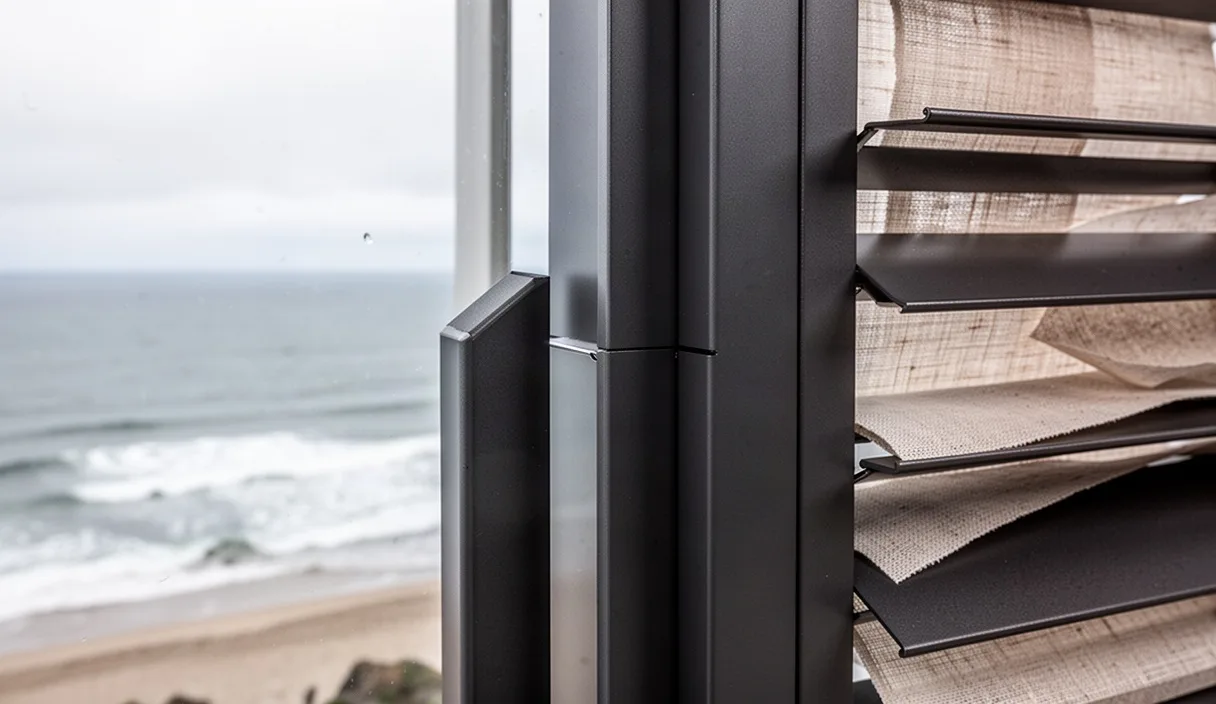
Powder-coated aluminum components deployed within three kilometers of an ocean coastline face an aggressive combination of airborne chlorides, cyclic humidity, solar ultraviolet exposure, and high surface temperatures. While aluminum naturally forms an amorphous protective oxide layer upon atmospheric contact, this barrier is vulnerable to localized breakdown when chloride ions penetrate surface defects. In the absence of an impermeable barrier coating and a resilient conversion base, chlorides cause pitting corrosion and filiform corrosion, an insidious filament-like degradation that creeps beneath the organic finish and lifts the cured film from the substrate.
Specifying powder-coated architectural aluminum for coastal installations requires moving beyond generic finish designations. Reliable barrier performance relies on an engineered system where alloy selection, mechanical extrusion geometry, chemical conversion pretreatment, and cured film thickness operate in tandem. This guide provides technical criteria, test standards, and specification language aligned with international standards such as ISO 12944, Qualicoat Seaside, and AAMA 2605 to ensure architectural components maintain their structural integrity and visual character in high-salinity zones.
Atmospheric Corrosivity Categories Under ISO 12944
The International Organization for Standardization establishes atmospheric corrosivity categories in ISO 12944-2, updated to distinguish between severe industrial conditions and open marine environments. Coastal projects generally fall into category C4 (High), C5 (Very High Marine), or the extreme category CX. Categorization does not depend solely on linear distance to the breaking surf. It is governed by mass deposition rates of airborne chlorides, ambient humidity, temperature shifts, and local wind vectors that transport maritime aerosols inland.
Category C4 denotes coastal areas with moderate salinity, often extending from one to five kilometers inland depending on terrain topography and onshore wind intensity. In category C4, airborne chloride deposition typically ranges between 60 and 300 milligrams per square meter per day. Category C5 applies to shorelines directly fronting the ocean, areas within several hundred meters of breaking waves where chloride deposition sits between 300 and 1500 milligrams per square meter per day. Category CX represents extreme marine zones, such as offshore rigs, coastal piers, and structures subjected to direct salt spray, where chloride deposition exceeds 1500 milligrams per square meter per day.
Microclimatic factors can force an individual elevation of a building into a higher corrosivity tier than the macroclimatic location indicates. Sheltered soffits, recessed window heads, and unwashed louvers frequently experience higher failure rates than windward facades exposed to open rainfall. Because rainwater naturally flushes surface-bound salts away, unwashed sheltered zones allow hygroscopic sea salts to accumulate, absorb nocturnal humidity, and form concentrated, highly conductive electrolyte solutions on the coating surface for prolonged periods.
Pretreatment Protocols: Acid Etch vs Alkaline Etch
Pretreatment is the most critical factor governing long-term powder coat adhesion on architectural aluminum alloys such as AA6060 and AA6063. Mill-finish extrusions carry uneven magnesium segregations, naturally occurring oxides, rolling lubricants, and airborne particulates. If the coater applies conversion chemistries directly over this native layer, micro-voids and weak boundary zones remain underneath the film, promoting filiform corrosion when moisture enters. Pretreatment chemically strips this layer to establish a consistent, clean base prior to conversion coating.
Alkaline etching uses a heated sodium hydroxide solution, typically maintained between 50 and 65 degrees Celsius, to aggressively dissolve the aluminum surface. This process exposes the underlying grain structure and removes surface defects. However, alkaline etching leaves behind insoluble intermetallic alloying elements, primarily iron, silicon, and copper, commonly referred to as "smut." The component must then pass through an acidic desmutting bath to dissolve these heavy-metal compounds. If the desmutting step is brief or the acid bath is contaminated, iron-rich precipitates remain on the surface, serving as galvanic initiation sites for corrosion beneath the subsequent powder film.
Acid etching relies on acidic fluoride or sulfuric-phosphoric chemistries operating at lower temperatures, usually between 25 and 40 degrees Celsius. Acid etching provides a milder, more uniform material removal rate that dissolves intermetallic inclusions alongside the aluminum matrix, leaving significantly less insoluble smut. However, single-stage acid etching often fails to strip deeper surface contamination on heavily oxidized extrusions stored improperly before processing.
The Qualicoat Seaside specification mitigates the shortcomings of both approaches by mandating a dual-etch pretreatment process. In this sequence, the extrusion undergoes an initial alkaline etch to remove substantial mass, followed immediately by an intensive acid etch. The combined dual-etch process must remove a minimum total of 2.0 grams of aluminum per square meter of surface area, with at least 0.5 grams per square meter removed during the acid phase. This ensures the total elimination of zinc, magnesium, and copper intermetallics from the surface before the application of the chrome-free titanium-zirconium conversion layer.
| Pretreatment Method | Etch Removal Rate | Removal Mechanism | Corrosion Risk Profile |
|---|---|---|---|
| Standard Alkaline Etch | 1.0 to 1.5 g/m² | Sodium hydroxide dissolution; requires desmutting | Residual intermetallic smut can initiate filiform corrosion if desmutting is incomplete. |
| Standard Acid Etch | 0.5 to 1.0 g/m² | Fluoride-based acidic dissolution; lower smut generation | Can leave heavy rolling skins or magnesium-rich layers intact on extruded surfaces. |
| Dual Etch (Qualicoat Seaside) | Minimum 2.0 g/m² total | Sequential alkaline dissolution followed by an acid stage | Provides the lowest risk profile by stripping all surface inclusions and alloying defects. |
Film Thickness Verification and Pinhole Testing
Dry film thickness (DFT) directly dictates the rate at which water vapor and ionic species diffuse through the thermosetting organic layer to reach the metal substrate. For coastal installations classified as C4 or C5, standard commercial powder thicknesses of 40 to 50 microns are insufficient. Architectural specifications must require a minimum local dry film thickness of 60 microns, with an overall average target between 75 and 90 microns for standard superdurable polyesters. For fluoropolymer systems complying with AAMA 2605, target thicknesses typically range between 55 and 75 microns depending on formulation.
Film thickness measurement must follow non-destructive eddy-current principles in compliance with ISO 2360 or ASTM D7091. Because powder coating naturally wraps around extruded profiles unevenly due to electrostatic Faraday cage effects, spot checks must target challenging profile areas: internal corners, re-entrant angles, screw flutes, and deep channels. Applicators must verify calibration against smooth, non-magnetic metallic reference shims that reflect the profile geometry of the extrusions under evaluation.
Dry film thickness alone does not guarantee a continuous barrier. Microscopic voids, known as pinholes or holidays, form when trapped air, outgassing volatiles, or chemical moisture rupture through the curing powder layer before cross-linking completes. In coastal zones, a single holiday allows saline electrolyte to pool directly against the treated aluminum, triggering localized pitting. Holiday testing must be executed in accordance with ISO 29601 or ASTM D5162:
- Low-Voltage Wet Sponge Testing: Used for total film thicknesses up to 500 microns. A cellulose sponge saturated with an electrolyte solution (tap water with a non-foaming wetting agent) passes across the cured surface at a rate not exceeding 300 millimeters per second. The tester applies an operating voltage between 9 volts and 90 volts direct current. When the wetting agent makes contact with the substrate through a void, an electrical circuit completes, triggering an audible alarm.
- High-Voltage Spark Testing: Reserved primarily for specialized high-build barriers or thick multi-coat assemblies exceeding 500 microns, where an electrical spark discharges across air gaps at calculated dielectric breakdown voltages. This method is rarely required for standard architectural profiles.
Edge Coverage and Geometry Risks on Sharp Extrusions
The failure of powder coating in coastal environments rarely begins in the center of flat surfaces; it initiates at edges, cut ends, and sharp corners. During the electrostatic powder application, the Faraday cage effect repels charged powder particles away from sharp external vertices and internal corners. Furthermore, during the thermal cross-linking cycle inside the curing oven, surface tension causes the molten polymer to pull back from sharp corners, thinning the liquid film before it vitrifies.
If an extrusion has a sharp, 90-degree corner with a radius under 0.5 millimeters, the dry film thickness at the apex can drop by 35 to 60 percent compared to adjacent planar faces. While the face might register an acceptable 80 microns, the edge may carry less than 25 microns of protective polymer. This thin edge permits early chloride entry, allowing filiform corrosion to track inward beneath the paint film.
Architectural drawings must explicitly mandate an edge radius of not less than 1.5 millimeters (and ideally 2.0 millimeters) on all exposed corners of custom aluminum dies. For standard stock dies with sharper edges, extrusions must undergo mechanical edge deburring or edge rounding before loading onto the pretreatment line.
Fabrication practices present equal exposure risks. Miters, factory cut ends, field cuts, drainage weep holes, and drilled fastener holes expose bare, un-pretreated, uncoated aluminum alloys directly to the elements. Miters must be sealed with a neutral-cure, non-conductive elastomeric sealant, and all field cuts or drilled holes must receive a barrier primer (such as an approved two-part epoxy primer or polyurethane touch-up coating) before mechanical fastening.
Periodic Washing Protocols to Maintain Warranty Validity
Corrosion warranties from powder manufacturers and applicators for coastal environments are conditional documents. They contain strict maintenance covenants requiring building owners to wash the coated components periodically and record the maintenance in a formal logbook. Failure to keep washing records invalidates warranty coverage in the event of filiform or peeling failures.
The required cleaning frequency depends on the corrosivity category and building location:
- Direct Sea-Facing Zones (Within 1000 meters of open shoreline): Cleaning must occur at intervals not exceeding three months.
- Coastal-Adjacent Zones (Between 1000 and 5000 meters inland): Cleaning must occur at intervals not exceeding six months.
- Sheltered, Unwashed Surfaces: Regardless of distance, surfaces that do not receive direct rainfall (such as overhangs, soffits, recessed door frames, and underside surfaces of balcony rails) must be cleaned manually every three months to prevent the dry accumulation of salt crusts.
Washing procedures must avoid harsh alkaline cleaners, abrasive scrubbers, and industrial solvents that degrade the polymer binder. Cleaning must be carried out using clean municipal water mixed with a neutral, non-abrasive detergent maintaining a pH between 5.5 and 8.0. The wash sequence begins with a low-pressure water rinse to float off gritty windblown silica and crusty salt deposits. Personnel must then use soft, lint-free cloths or non-abrasive soft-bristle brushes to wipe down the surface using light mechanical pressure. Once dirt and salt crusts are emulsified, workers must rinse the components thoroughly with clean fresh water to clear all surfactant residues, finishing with a squeegee or microfiber wipe-down to prevent hard-water mineral spotting.
Common Mistakes
- Assuming High-Performance Powder Solves Poor Pretreatment: Specifying an advanced resin, such as an AAMA 2605 fluoropolymer or a superdurable Class 2 polyester, will not stop corrosion if the underlying aluminum receives an inadequate single-stage acid wash with an etch removal rate below 1.0 gram per square meter.
- Overlooking Salt Buildup Under Soffits: Assuming that areas sheltered from rain and sunlight require less maintenance. In reality, the lack of natural rain washing leads to heavy salt consolidation and rapid corrosion initiation on leeward and covered elevations.
- Specifying Razor-Sharp Extrusion Geometry: Permitting extrusions with external corner radii below 1.0 millimeter, which systematically starves vertices of sufficient dry film thickness during the powder reflow process.
- Leaving Cut Edges and Drill Holes Bare: Cutting extrusions to length on site or drilling fastener holes through cured profiles without applying an approved touch-up sealant or barrier primer to raw aluminum surfaces.
- Ignoring Applicator Certification: Sourcing material from coaters lacking third-party certification, such as Qualicoat Seaside or AAMA-accredited coater licenses, which require daily chemical bath titrations and documented quality assurance audits.
Specification Checklist and Implementation Steps
To ensure robust corrosion protection on aluminum facades in coastal microclimates, structural engineers, facade consultants, and specifiers should follow this sequential workflow:
Establish Site Corrosivity and Geometry: Review the project site on topographic maps to determine proximity to coastlines and prevailing marine winds. Mark all elevations as C4, C5, or CX according to ISO 12944. Check all extruded profile drawings to verify that external corner radii meet or exceed 1.5 millimeters.
Define Pretreatment and Chemistry: In project specifications, disallow generic clean-and-coat clauses. Explicitly specify a dual-etch alkaline/acid process complying with Qualicoat Seaside protocols, with a verified mass removal rate of at least 2.0 grams per square meter, followed by a certified chrome-free conversion layer.
Set Film Performance Benchmarks: Reference either Qualicoat Class 2 / Seaside or AAMA 2605 performance tiers. Mandate that dry film thickness meet a 60-micron local minimum, with holiday porosity testing executed in accordance with ISO 29601 at a low-voltage threshold between 9 and 90 volts on random factory batch samples.
Detail Assembly and Joint Protection: Require factory miters, field cuts, and structural penetration edges to be treated with compatible zinc-free or epoxy barrier sealers. Specify non-conductive isolation gaskets, such as EPDM or neoprene, beneath stainless steel fasteners to eliminate galvanic coupling between dissimilar metals.
Finalize Owner Maintenance Requirements: Draft an operations and maintenance manual section that details washing schedules, non-alkaline cleaning chemicals, water-pressure limitations, and logbook formats necessary to keep warranty protections in force. For high-density projects located directly along exposed marine surf, consult a qualified facade engineer or corrosion specialist to review connection details and local atmospheric deposition data.